Modular Conveyor Belt Series 2025: Versatility for Curved Transport and Food Products
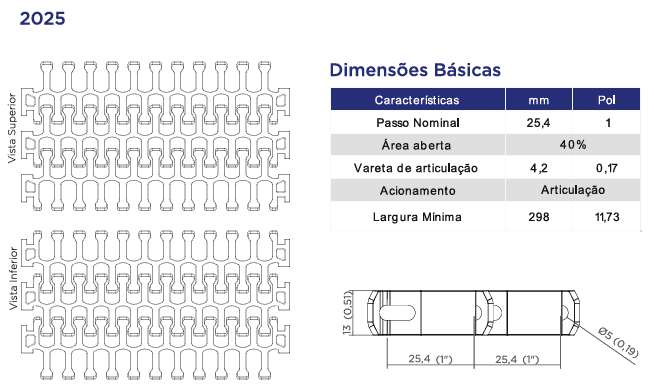
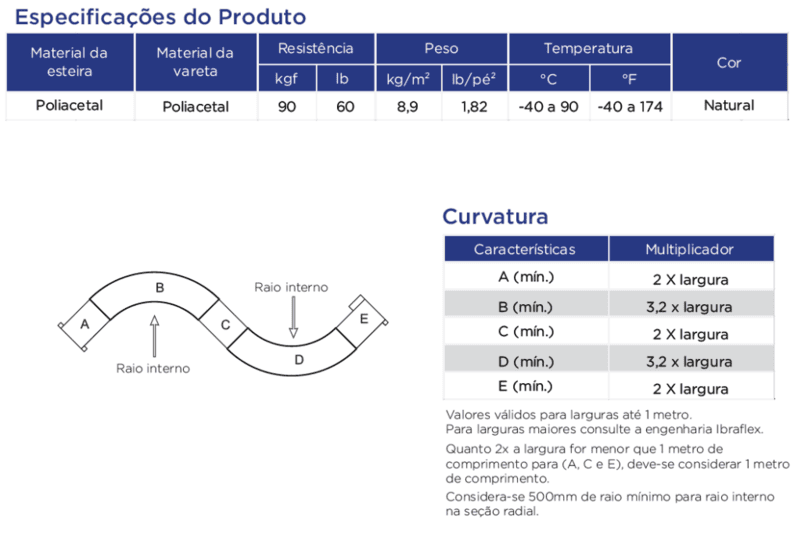
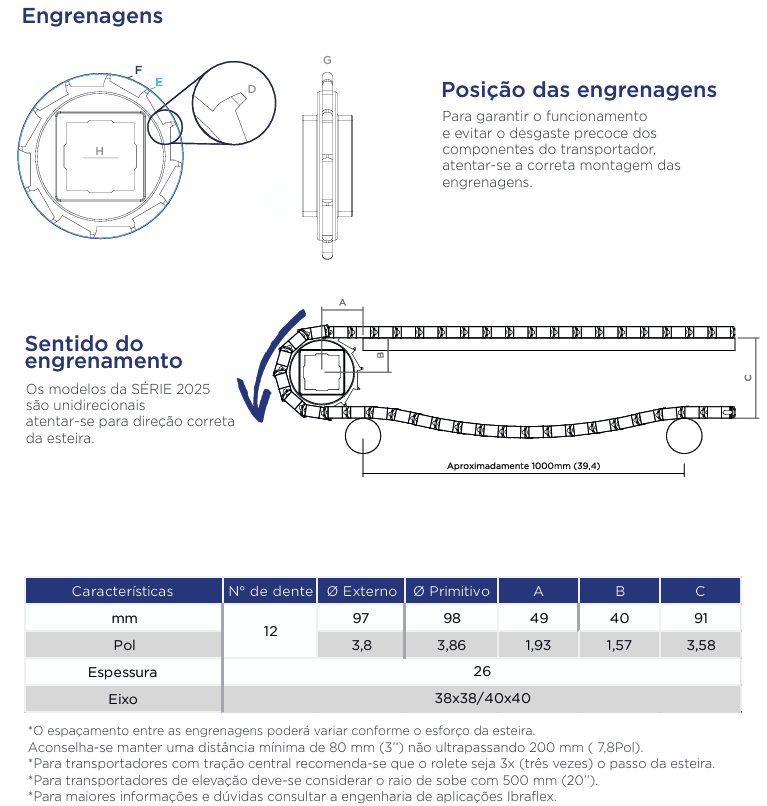
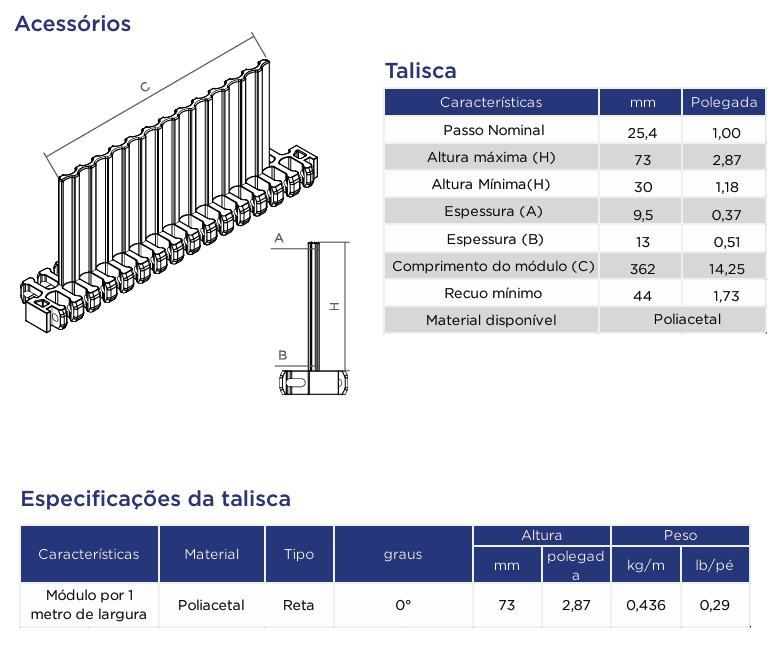
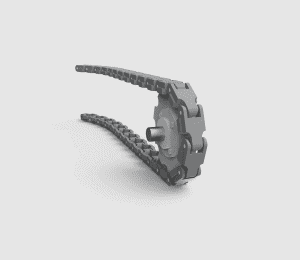
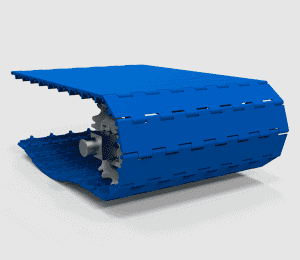
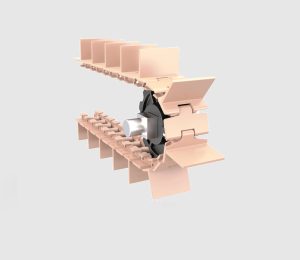
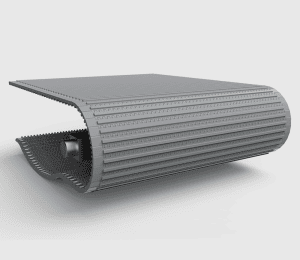
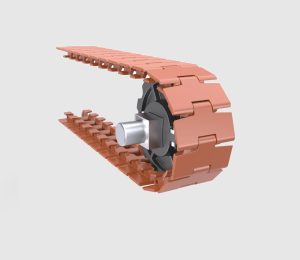
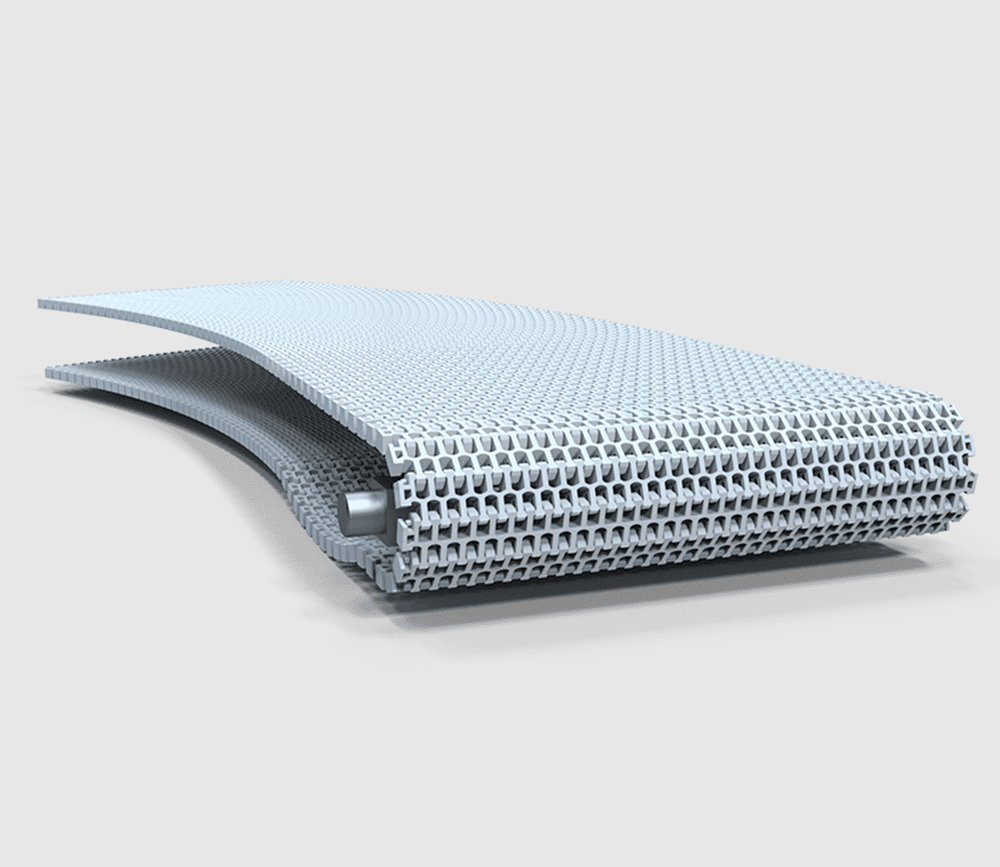
Ibraflex Series 2025 Modular Conveyor Belt was designed to meet multiple transportation needs in the food, beverage and logistics industries. With a nominal pitch of 25.4 mm (1″), it is ideal for transporting raw, processed, or packaged products. Its design allows for curved paths, ascents or descents, with or without cleats, ensuring efficiency in complex processes.
Applications
- Food Industry: Conveyor belts for fresh, packaged or processed products.
- Logistics Lines: Moving boxes along curved paths or inclines.
- Industrial Systems: An effective solution for processes that require flexibility and precision.
Why choose Series 2025?
- Application Flexibility: Handles curved paths, inclines, and declines with excellent performance.
- Durable Construction: Made with polyacetal, ensuring durability and reliability.
- Wide Open Area: 40% open area for greater ventilation and drainage, ideal for food applications.
- Compact and Light Weight: Minimum width of 298 mm (11.73″) and weight of 8.9 kg/m² (1.82 lb/ft²).
Ibraflex 2025 Series combines lightness, strength and adaptability, making it the perfect choice for applications that demand efficiency on challenging paths.
(Previously F25 series)